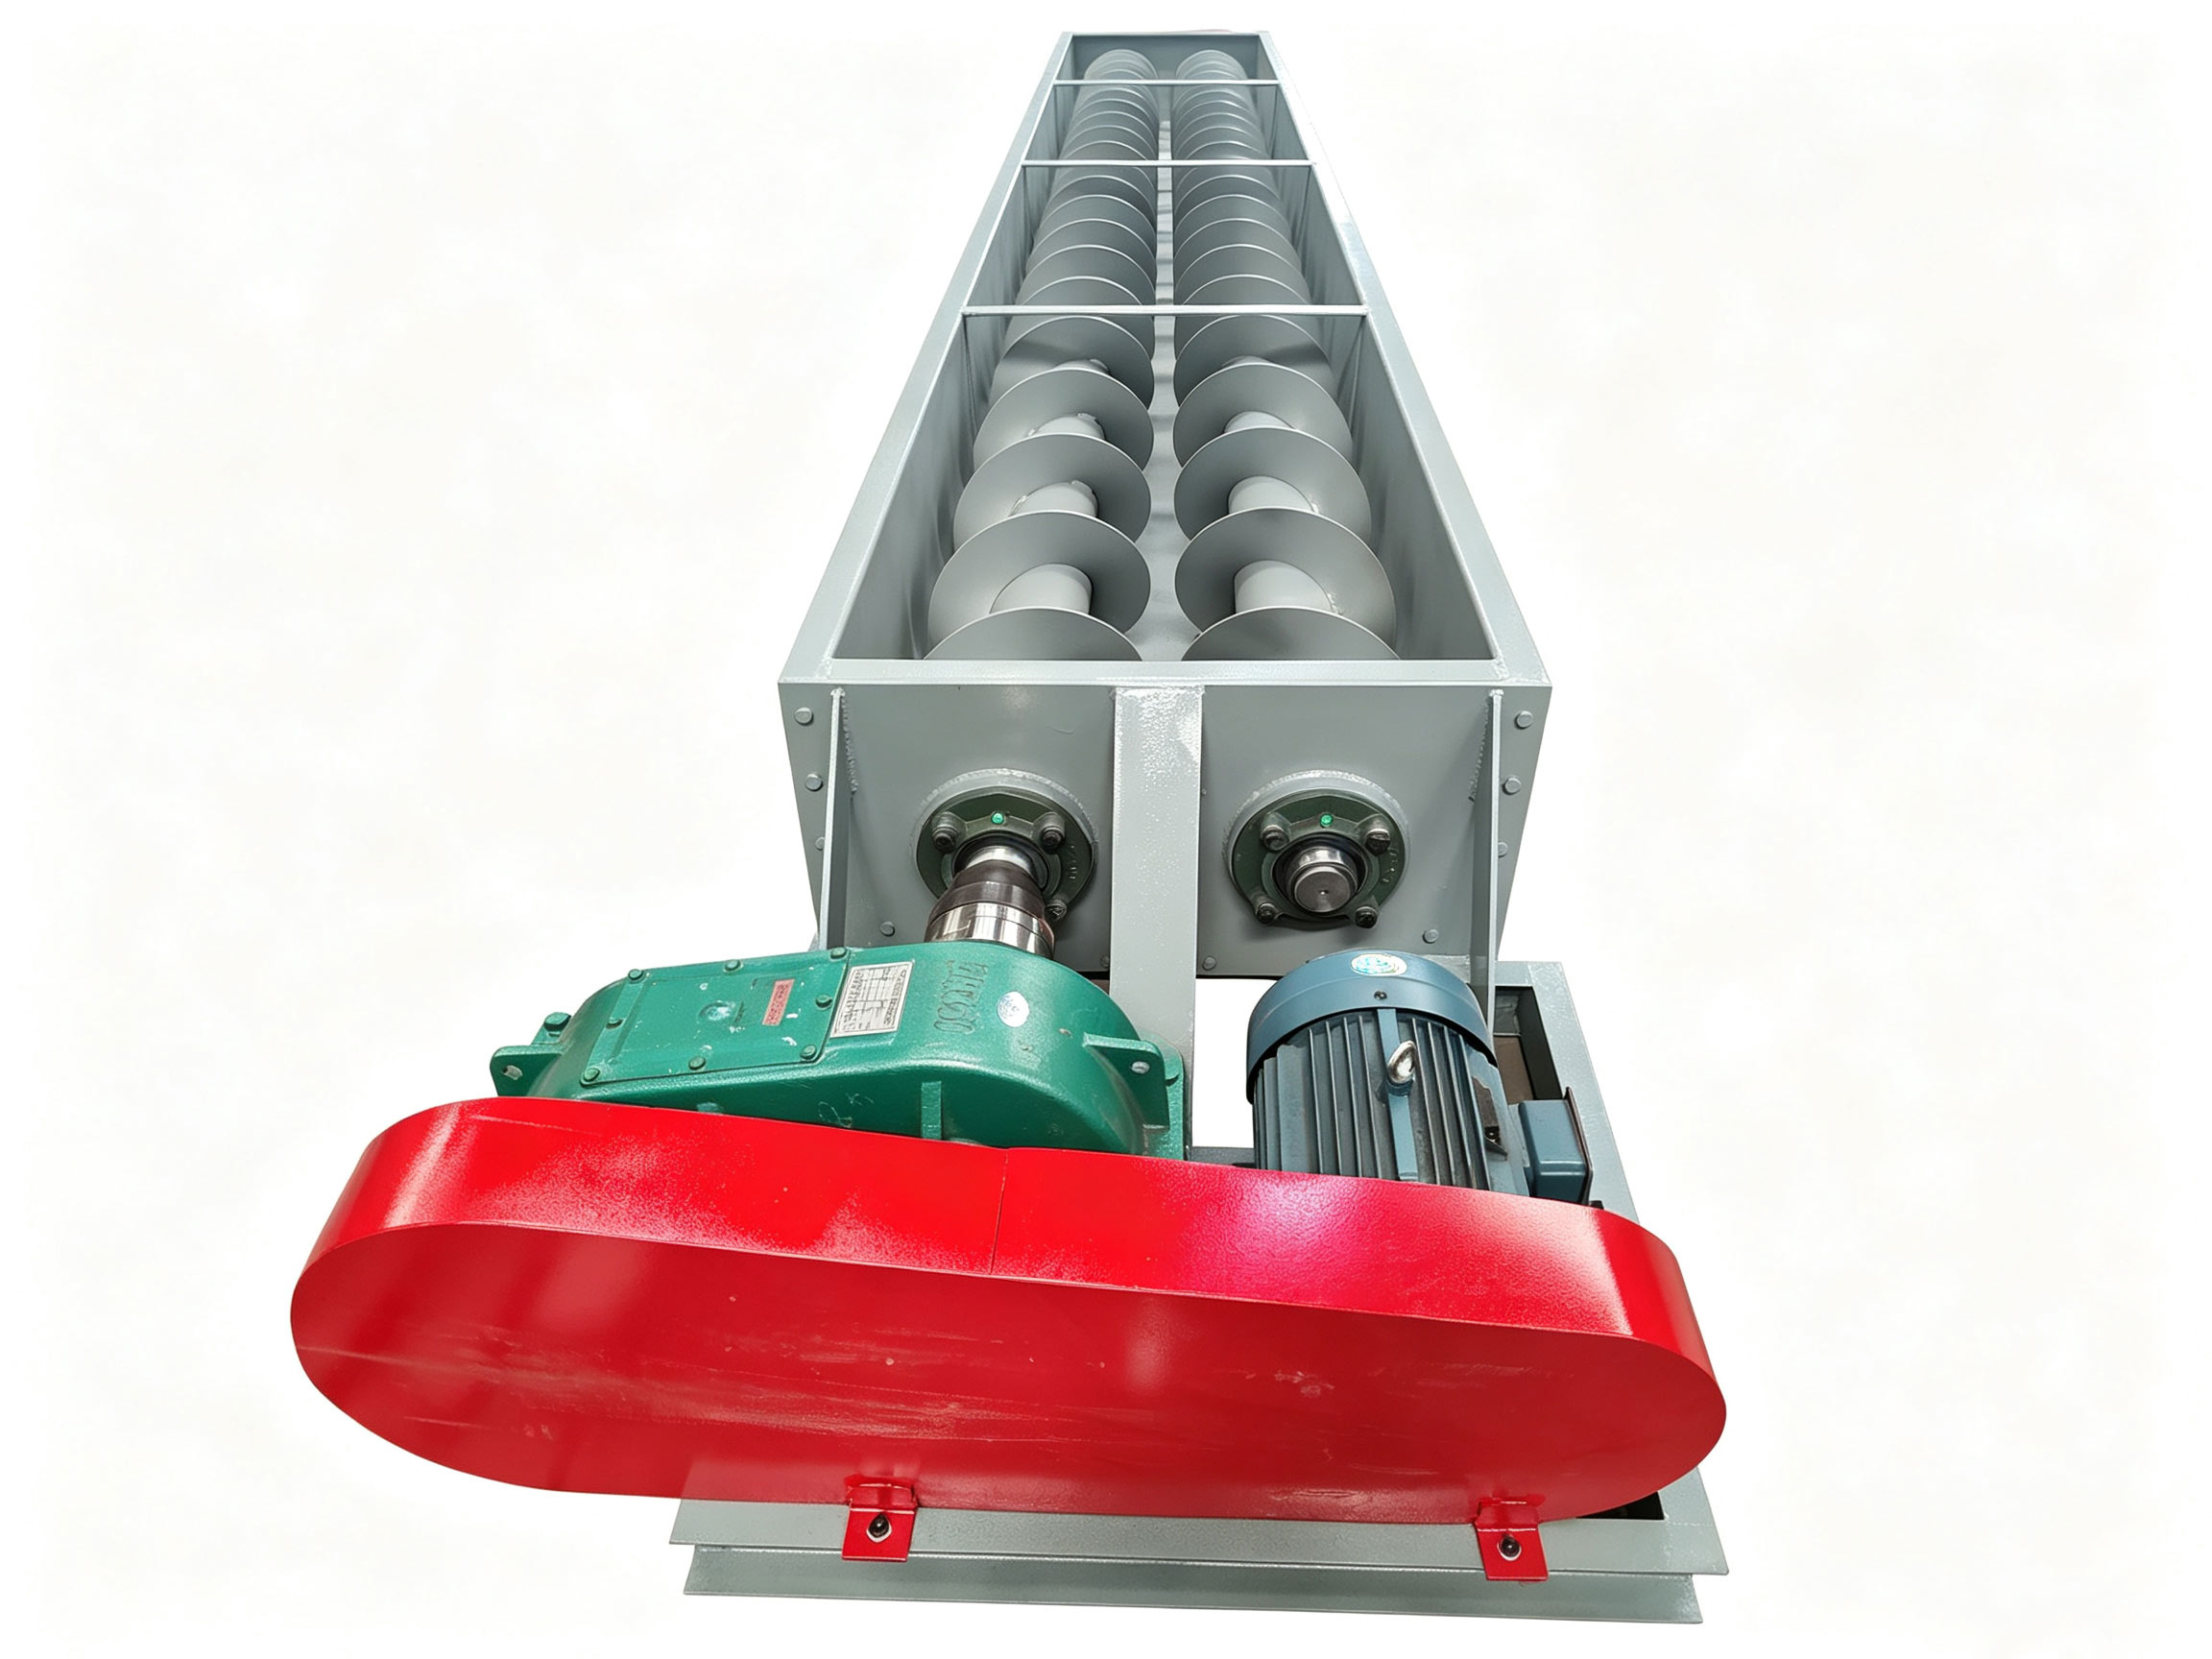
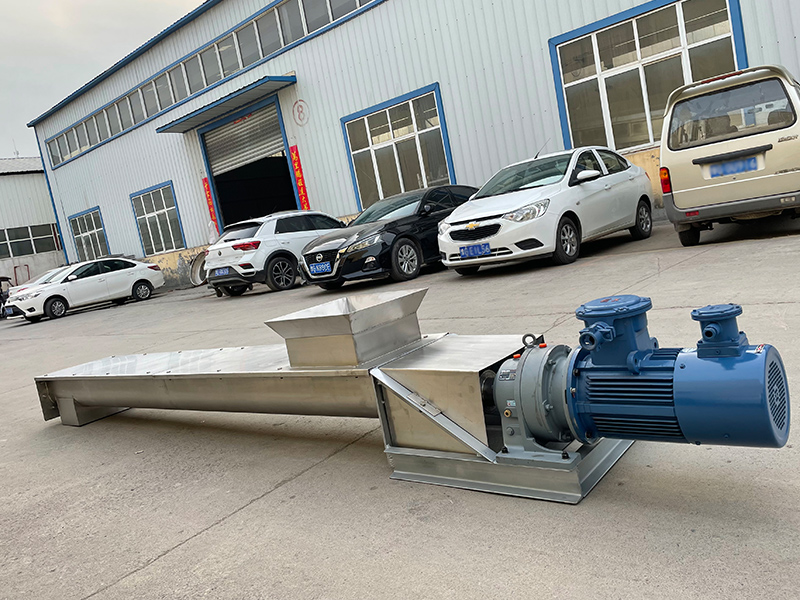
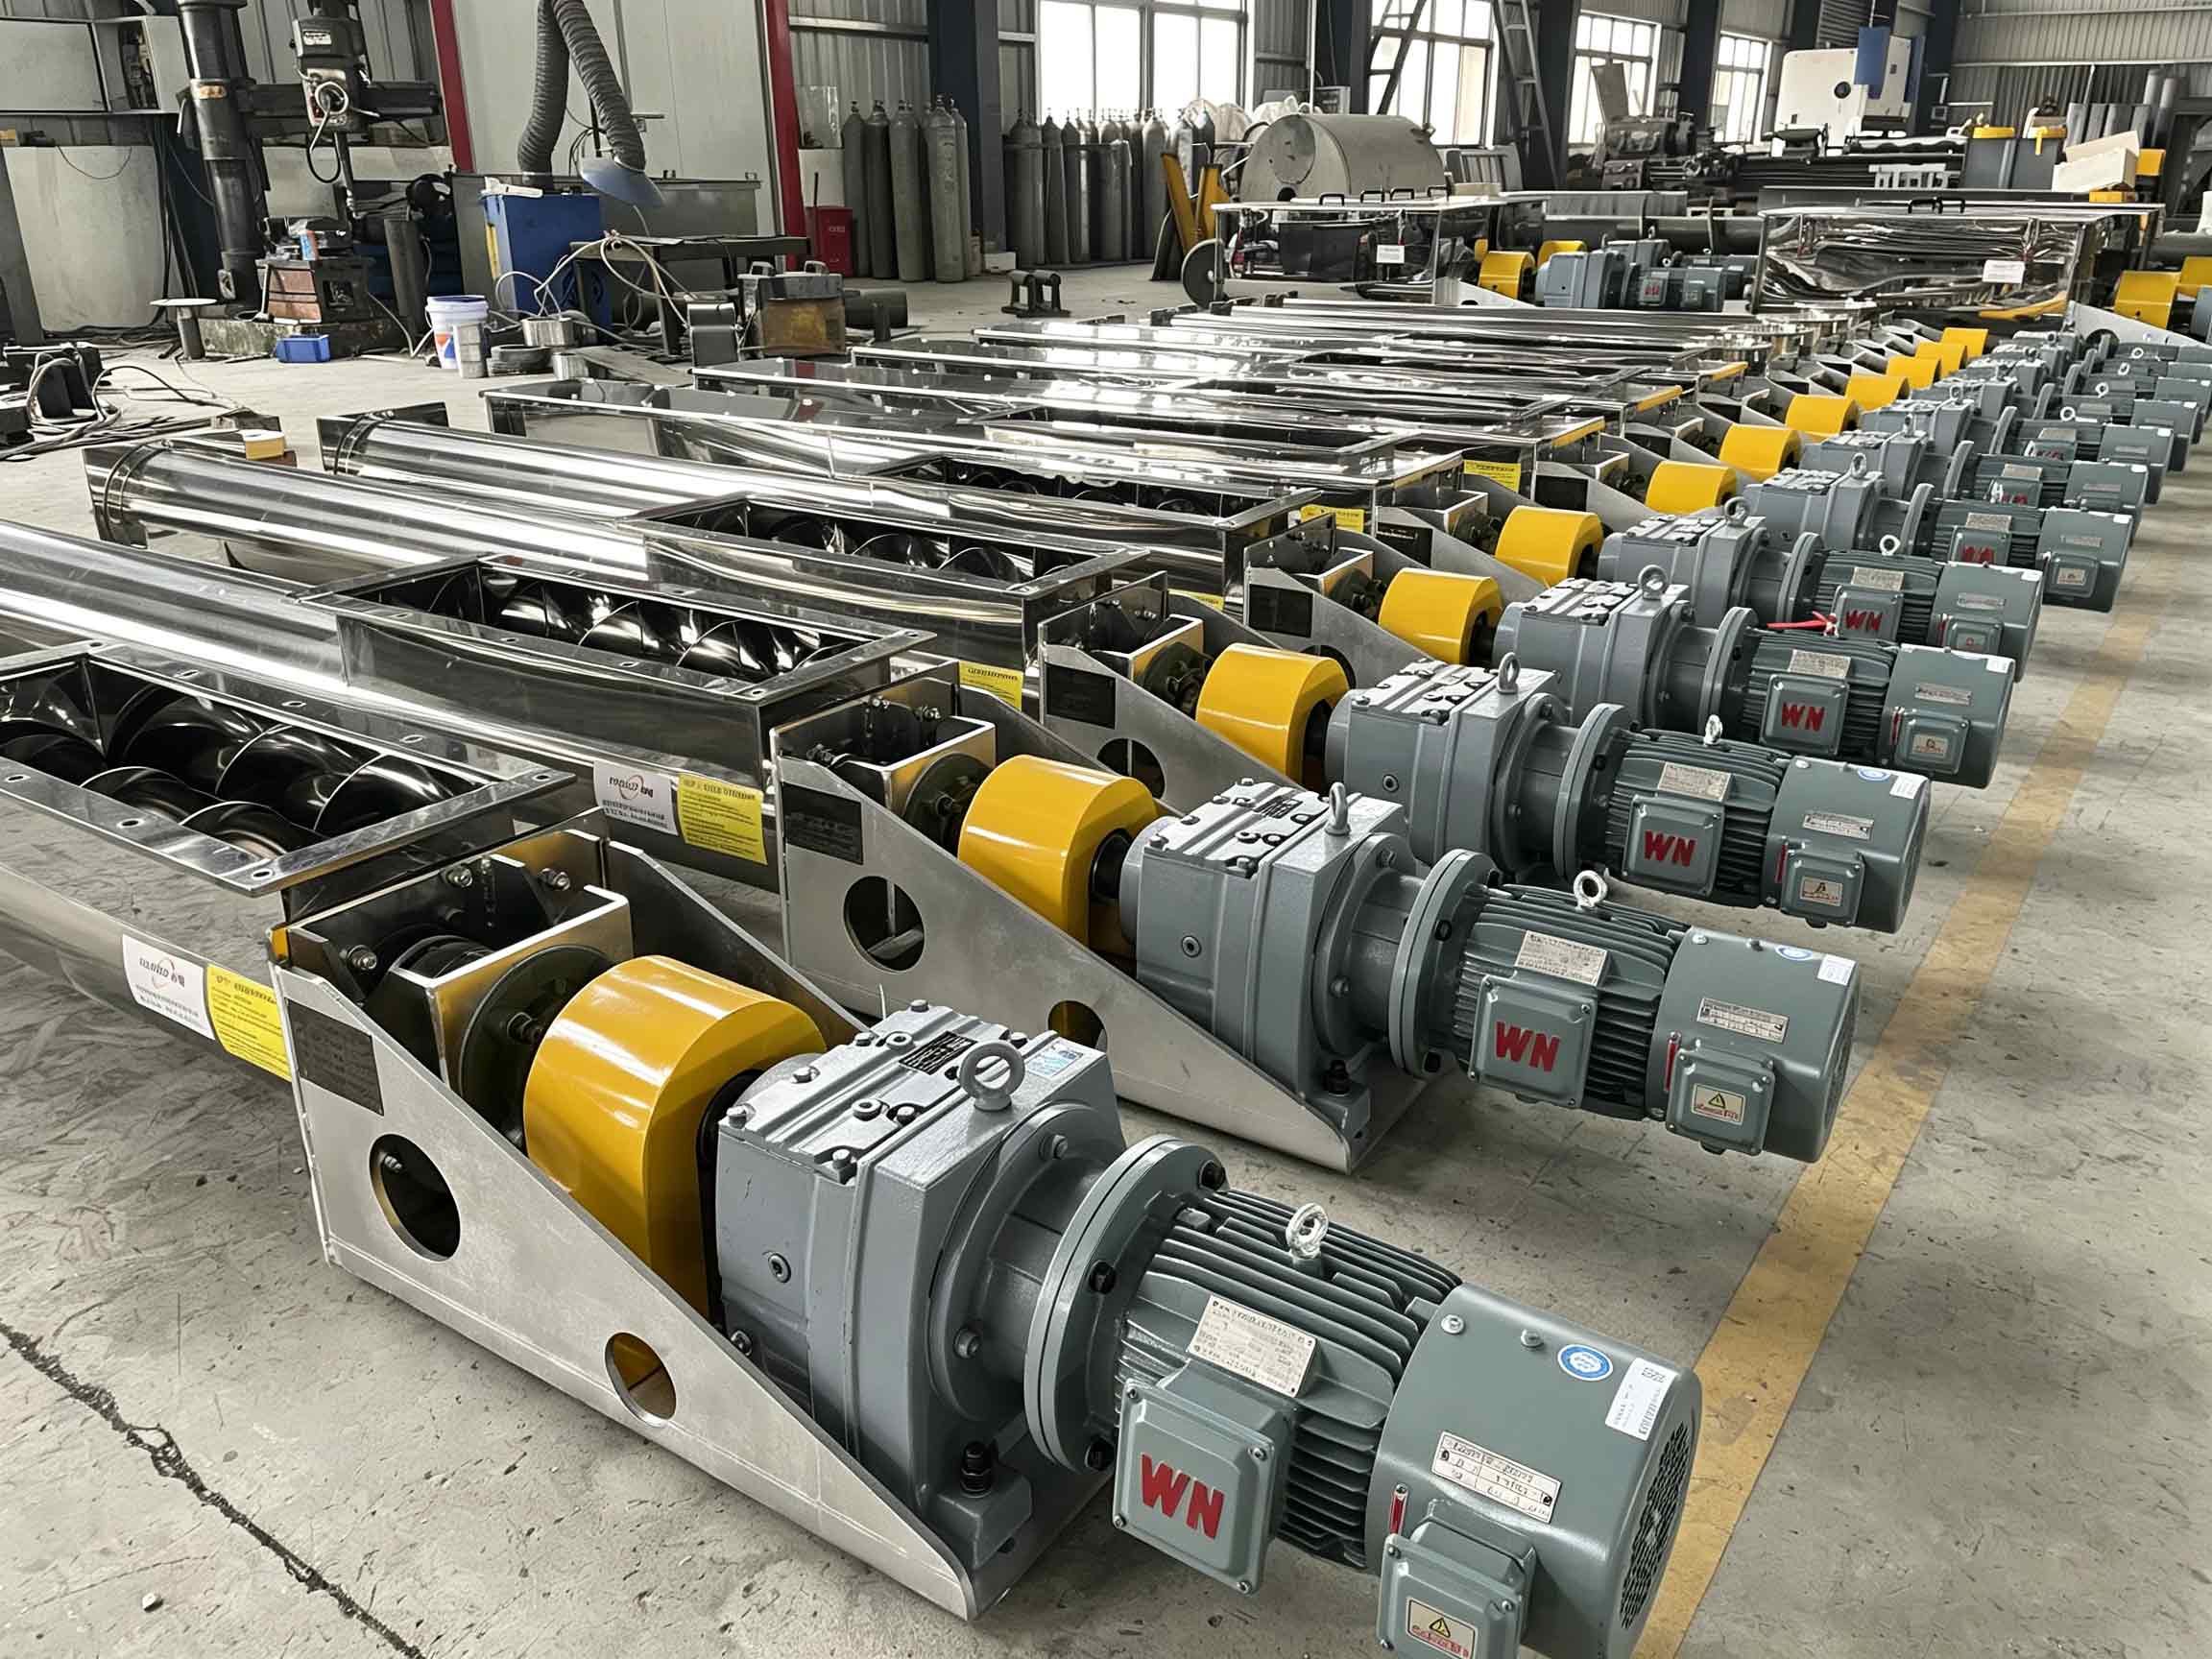
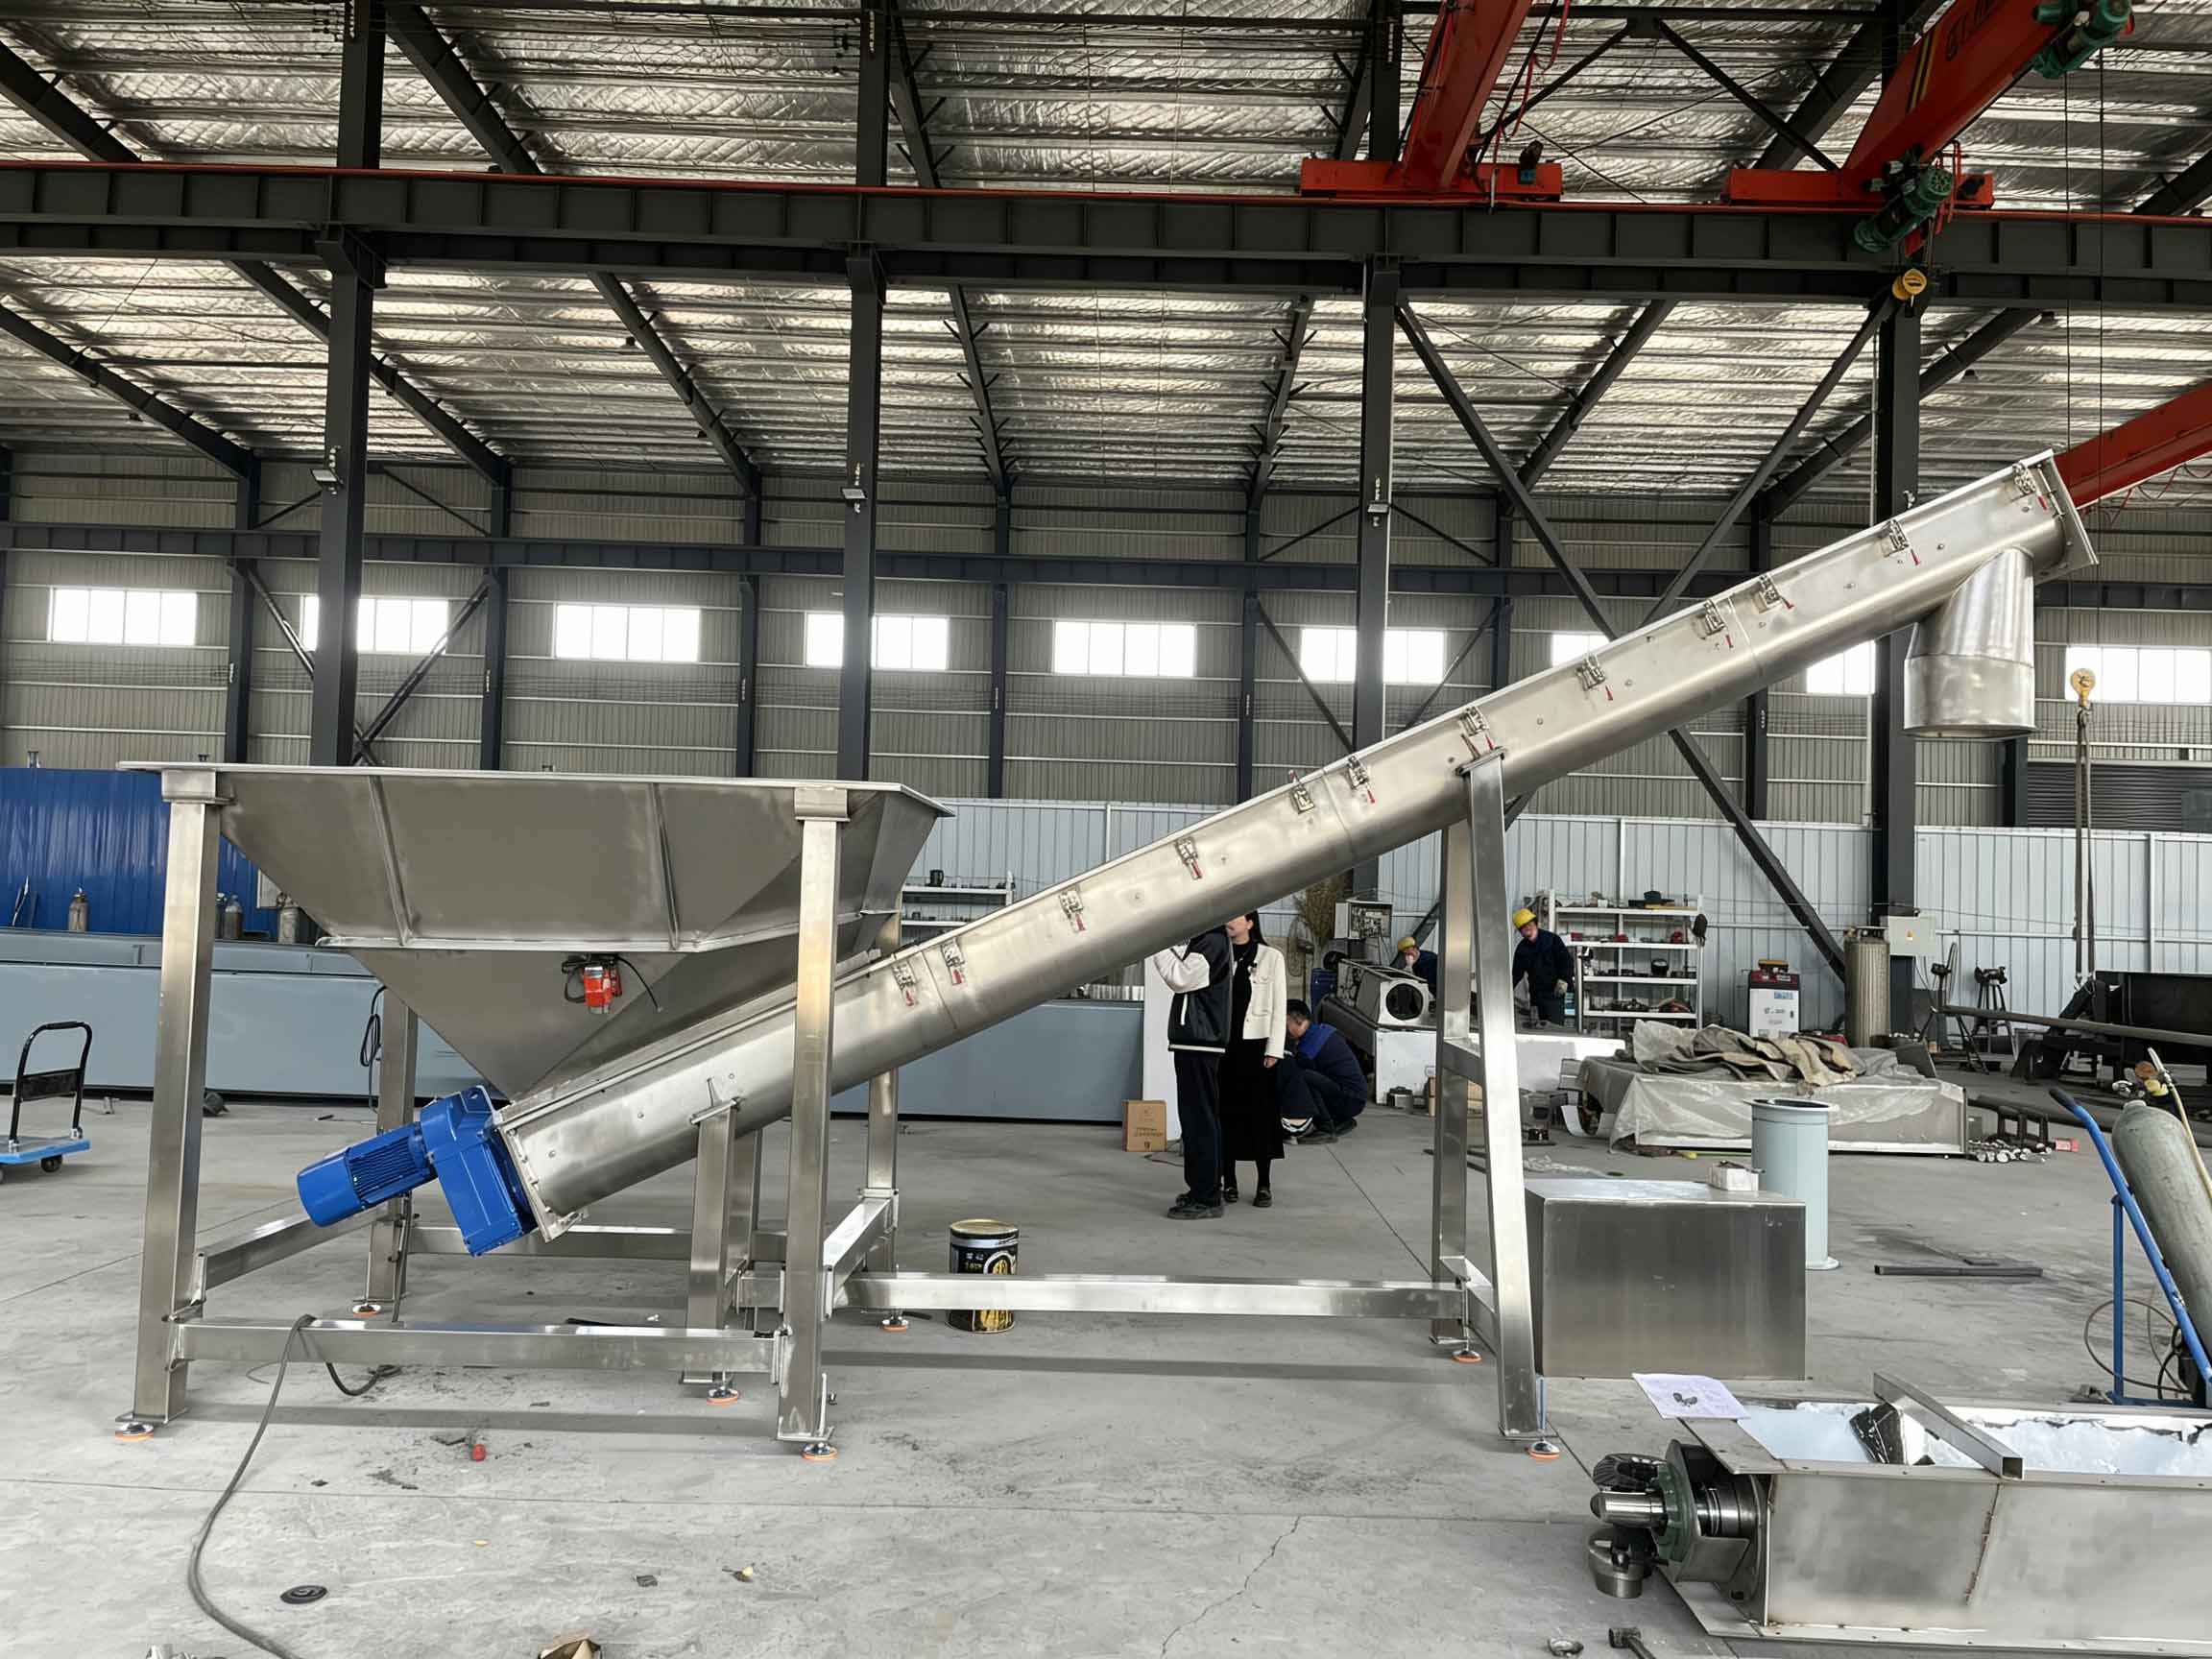
Twin-shaft Screw Conveyor
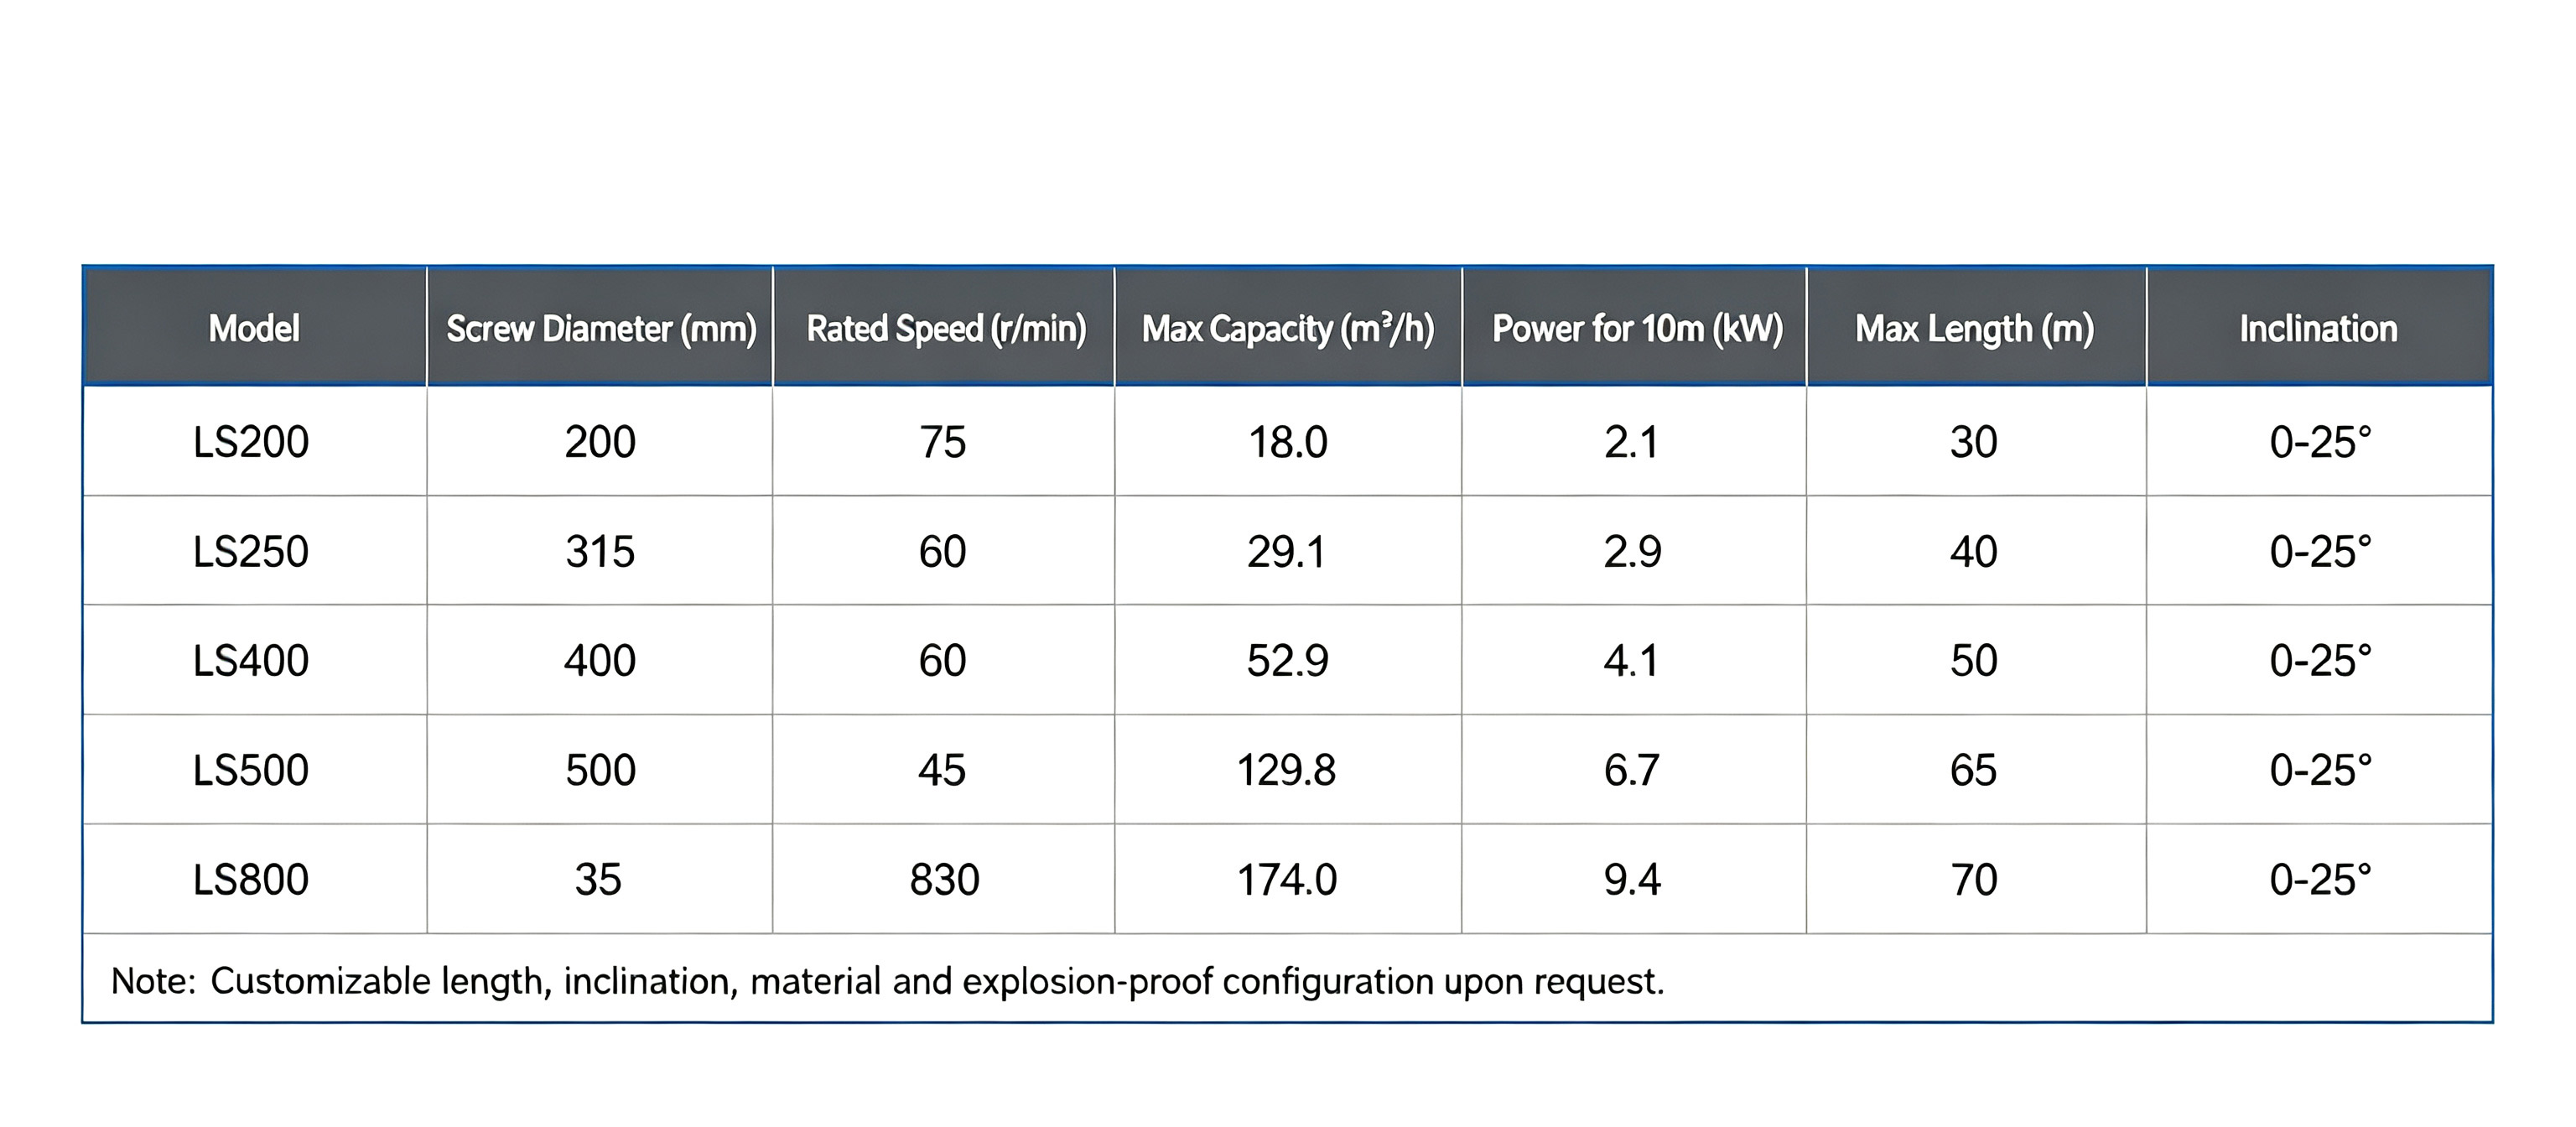
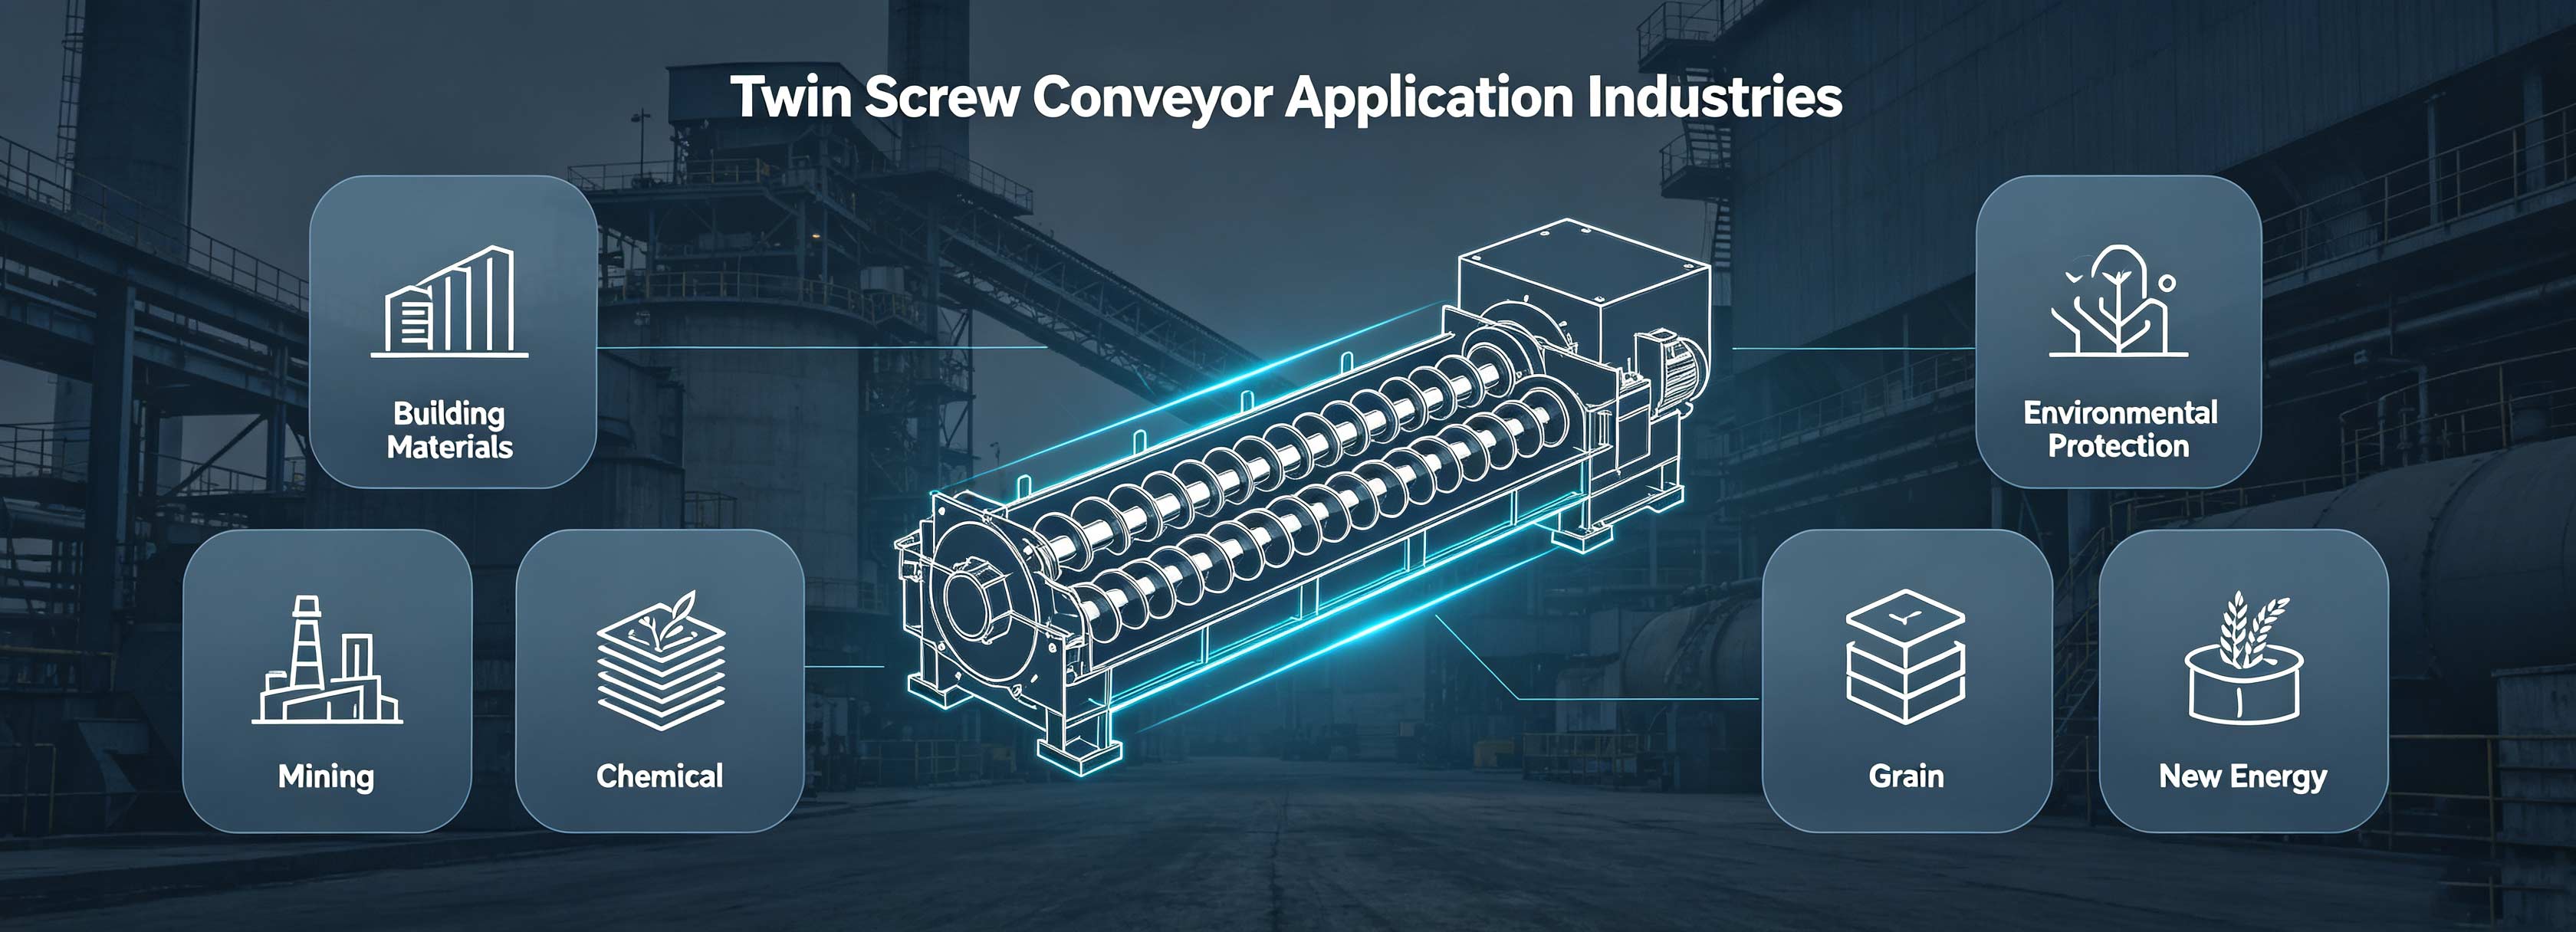
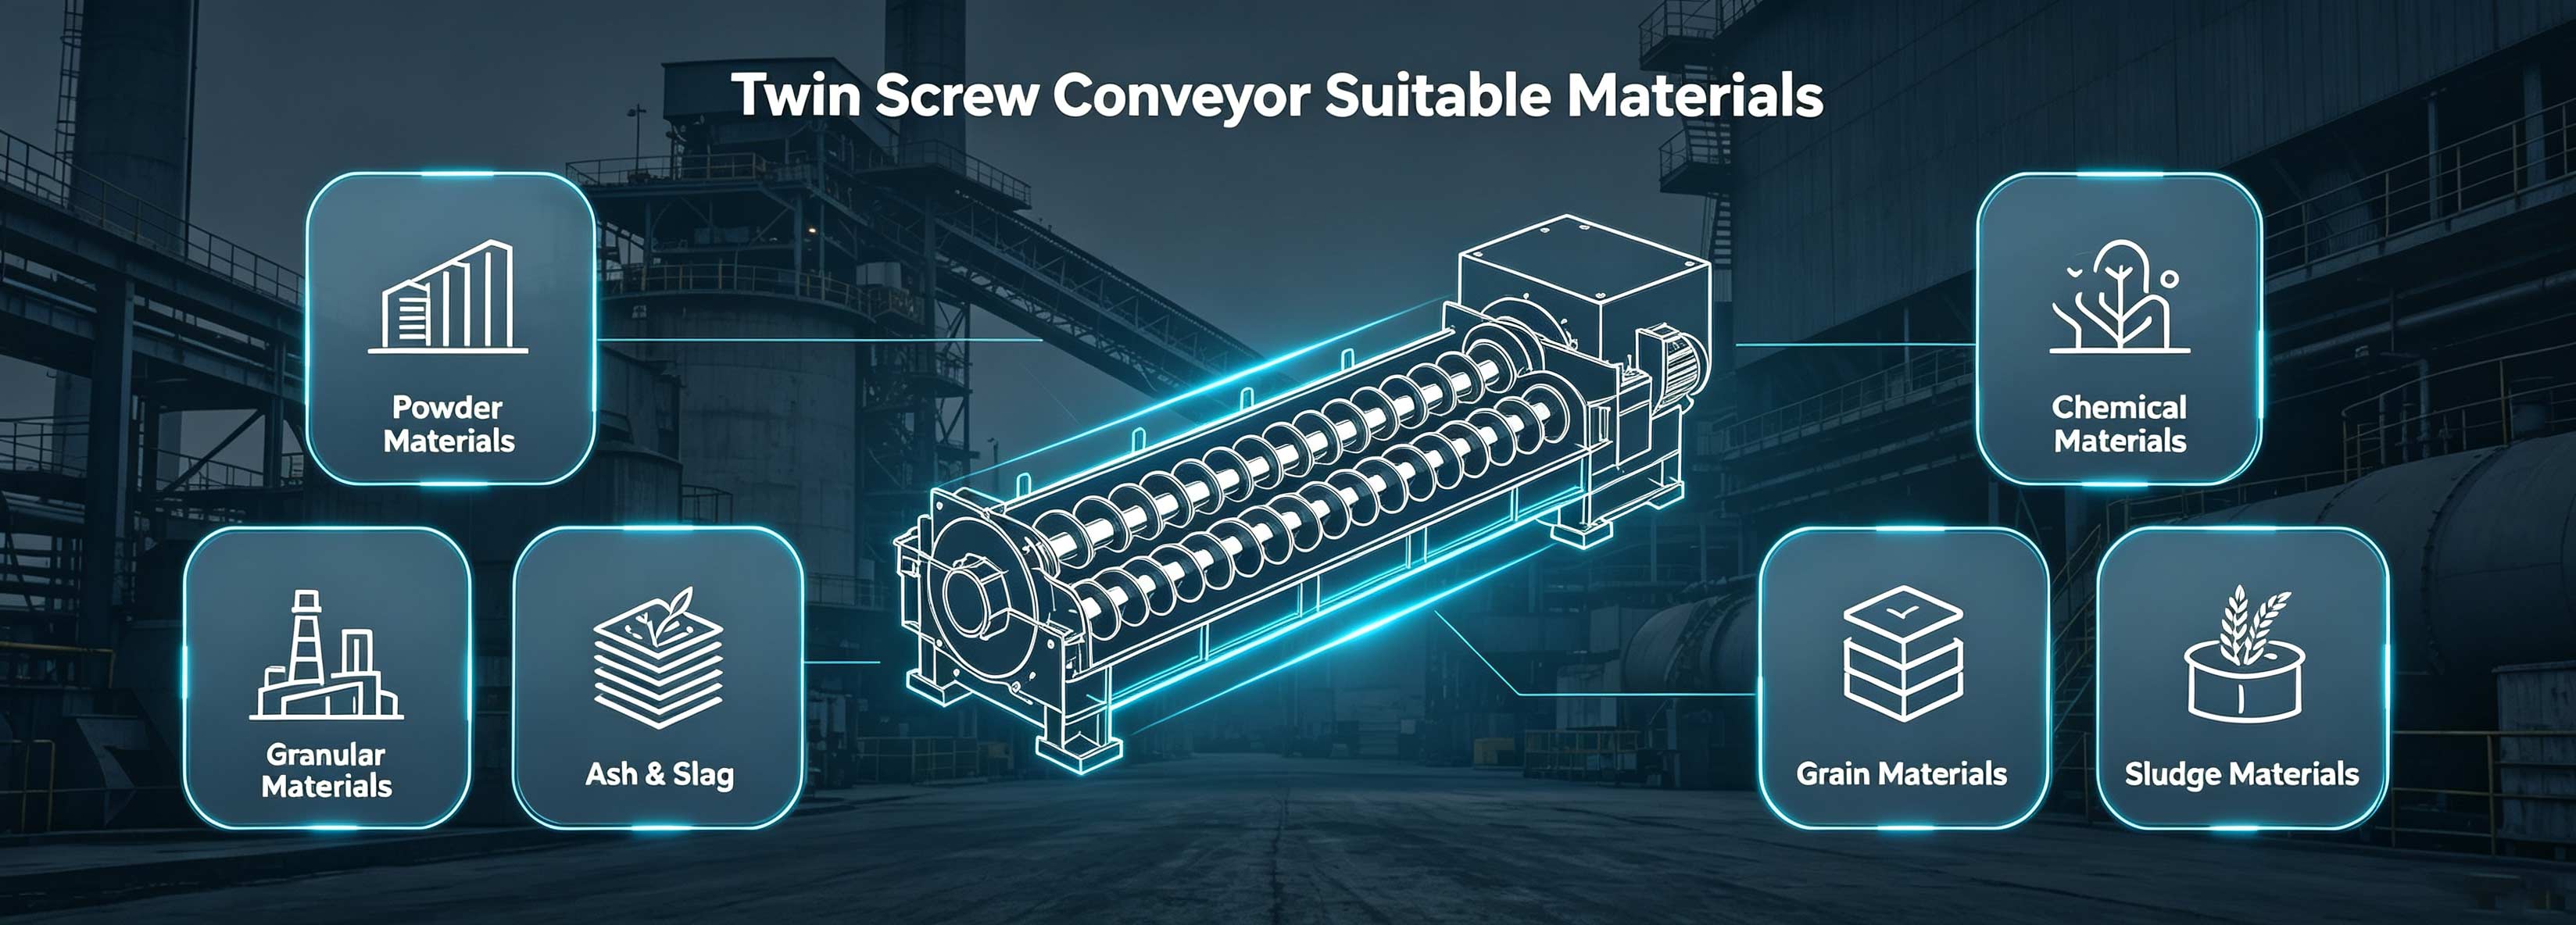
The double-shaft screw conveyor is a high-efficiency and multi-functional continuous conveying equipment. Different from traditional single-shaft screw conveyors, it is equipped with two counter-rotating screw shafts, integrating multiple functions including conveying, stirring, mixing, crushing and discharging. It is divided into double-shafted and double-shaftless structures. With a fully enclosed trough design, it can stably convey powdery, granular and block materials, and is also suitable for complex materials with high viscosity, entanglement and impurities. Widely used in mining, building materials, chemical industry, environmental protection, grain, metallurgy and other industrial fields, the equipment supports horizontal and small-inclination conveying (maximum inclination ≤25°). It features dust-free operation, zero material leakage and environmental protection. Its conveying capacity is 1.5-2 times that of ordinary single-shaft conveyors, supporting long-distance and large-flow continuous operation, serving as core equipment for industrial material conveying and pretreatment.